Guide
Why Almost Full Is Still a Packaging Problem
Learn how to separate foam height from net contents, sample a packaging run, and investigate carbonated beverage short fills with confidence.
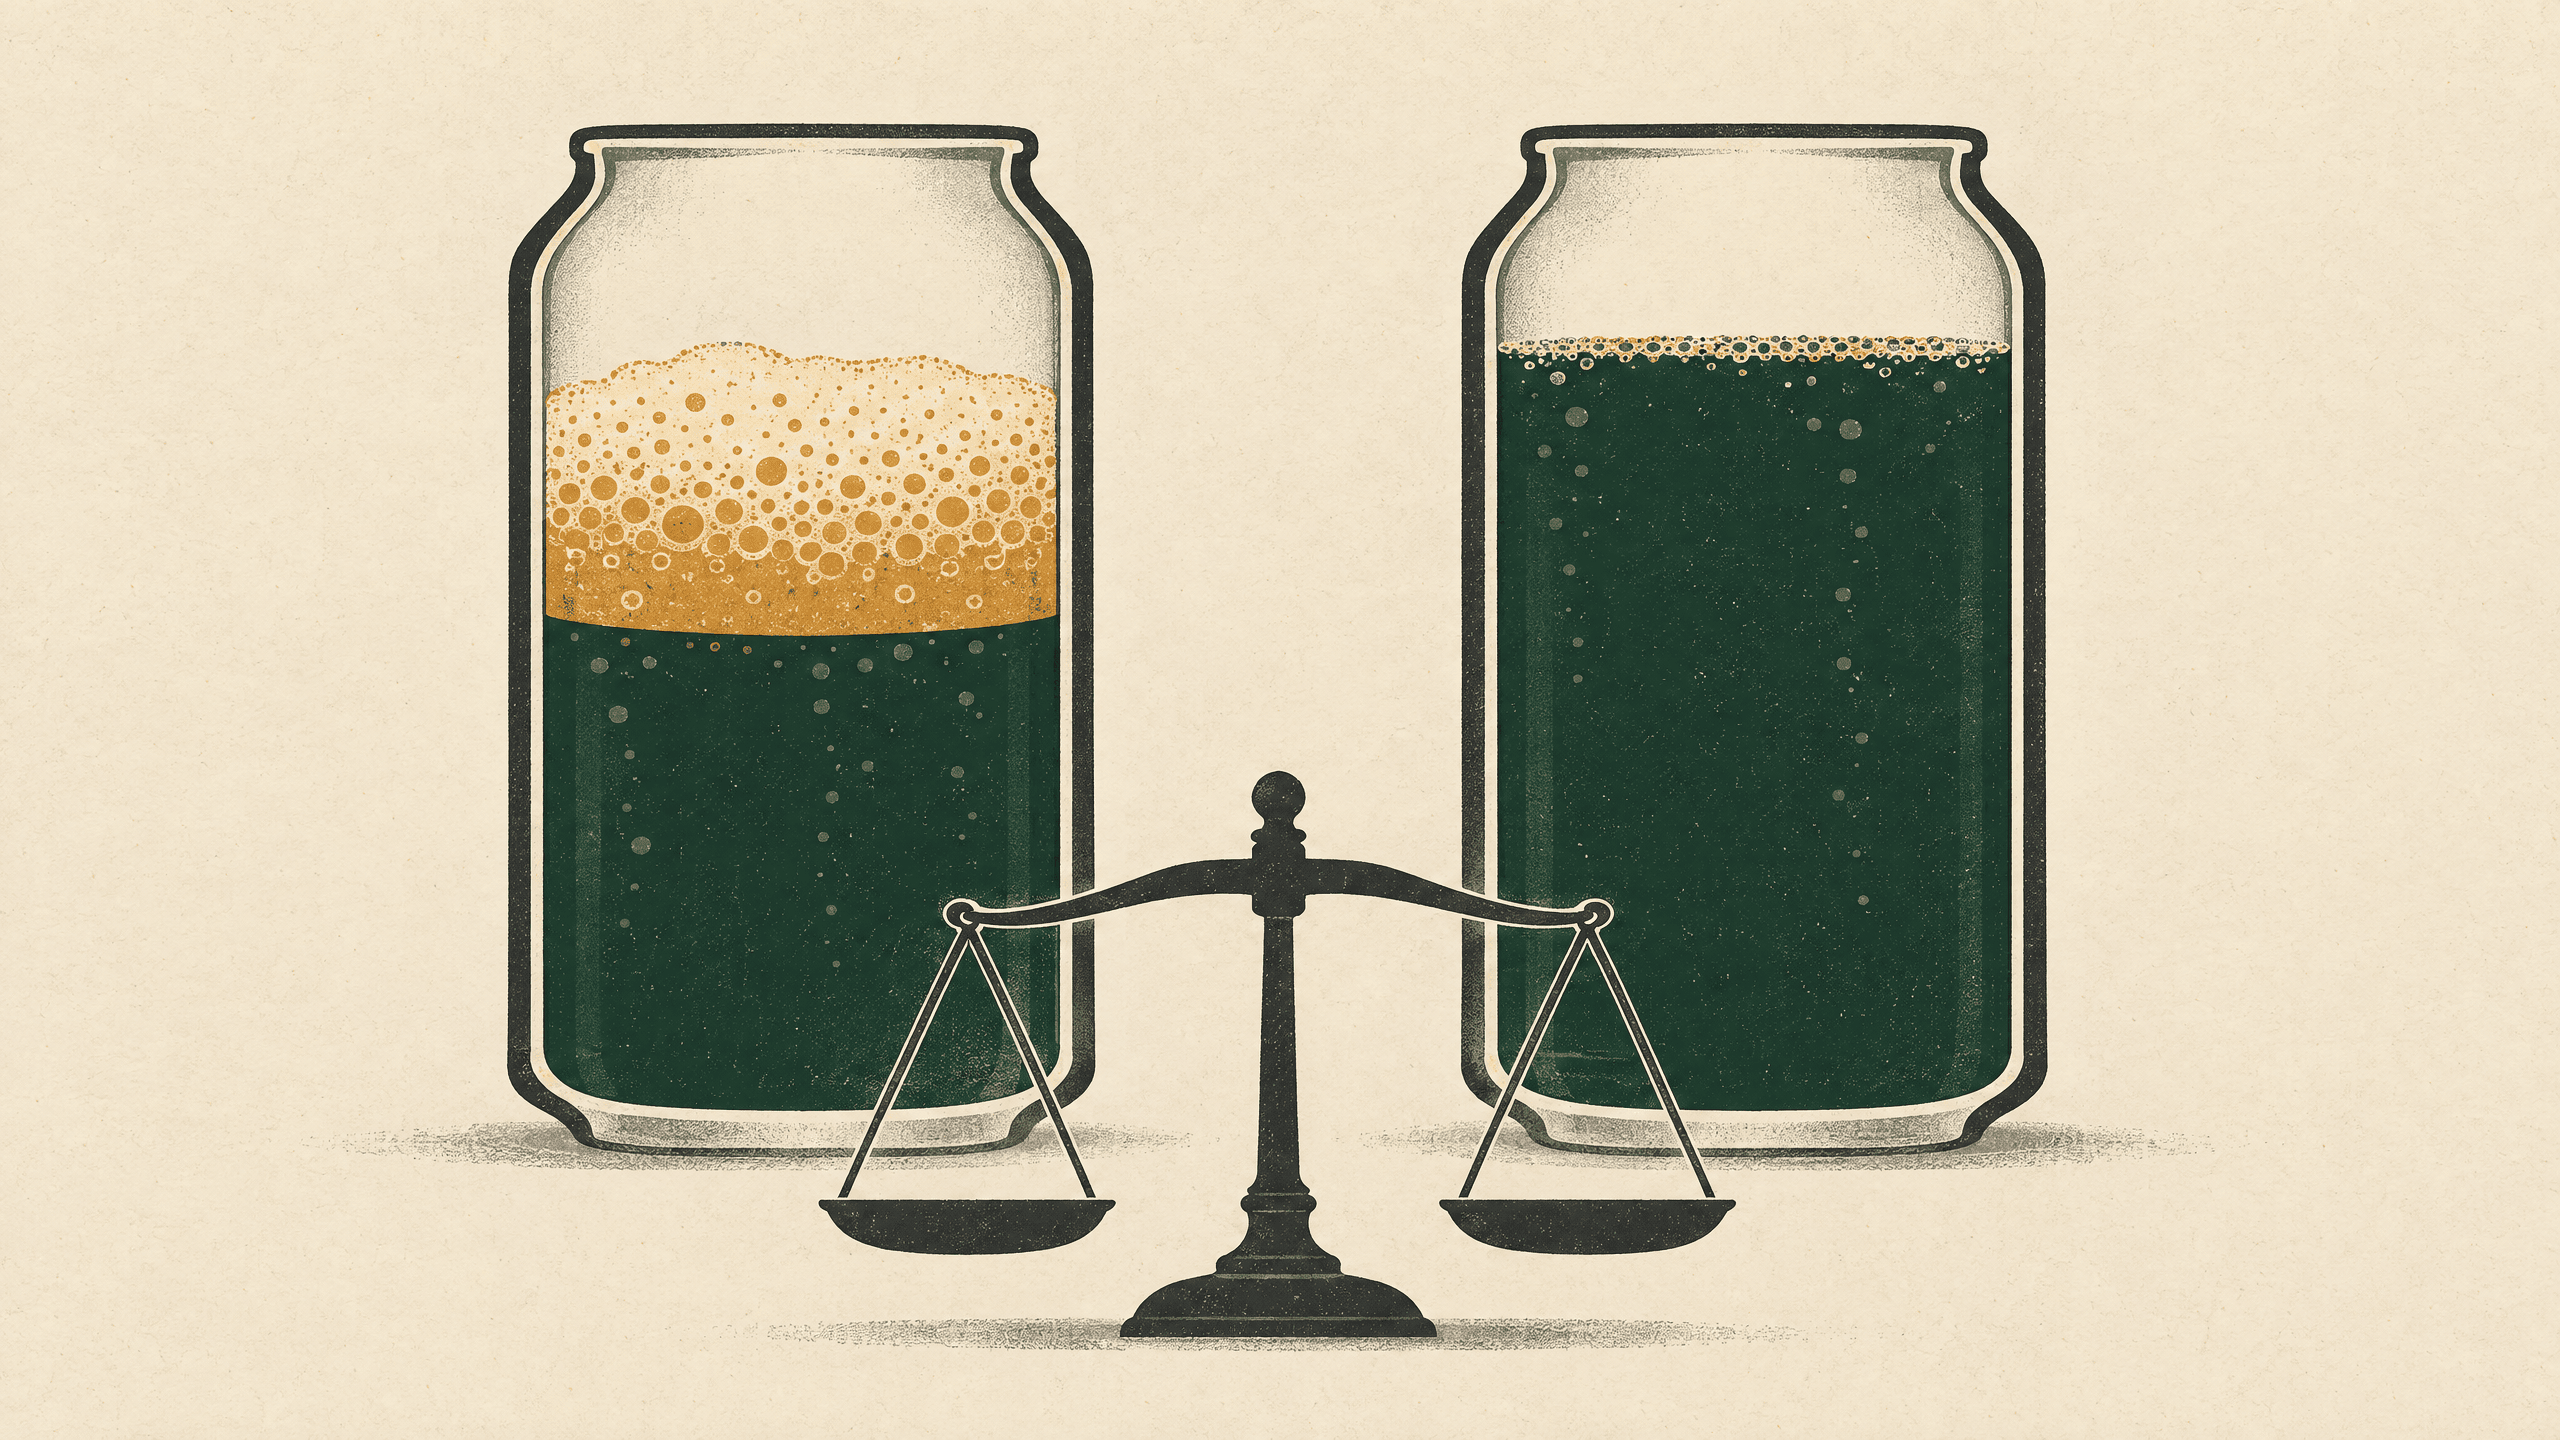
An almost-full can or bottle is easy to wave through when the line is busy. But repeated short fills in beverage packaging deserve a closer look. They can mean lost product, uneven presentation, or a process that is drifting while everyone is watching the foam instead of the contents.
The useful distinction is simple: foam height is not net contents. A package can look generous at the moment of fill because a foam cap has reached the intended level, then look short after the bubbles settle. Carbon dioxide can break out into bubbles as conditions change, and foam stability also varies with the beverage’s composition. Beer, cider, kombucha, seltzer, and other small-batch drinks will not all behave the same way.[1]
That does not make the visual result irrelevant. It makes it a clue, rather than the verdict. The question is whether liquid product is consistently reaching the declared net quantity after the package and its closure are accounted for.
Start with a measured answer
A reliable check is usually gravimetric: weigh a filled, closed package, then subtract the appropriate tare. Tare is not just an empty can or bottle; it is the packaging material your method says belongs in the calculation, including the closure where applicable. The result is net product mass.
Use a scale that is suitable for the check and maintained within your measurement system. NIST’s package-testing guidance calls for calibrated measurement equipment and explicitly calculates net weight as gross weight minus tare. Its official-inspection approach also treats tare as a sampled measurement, not a number to guess once and forget.[2]
If your package is labelled by volume, a mass check can still be useful, but only with a validated density for the actual product and method. Density turns mass into volume; it is not a universal conversion factor for every SKU, batch, or measurement condition. Confirm that it remains appropriate when the formulation, process, or product condition changes. If density varies materially between samples, investigate rather than forcing a neat conversion.
Do not borrow a legal fill tolerance from a different market or product category. Net-quantity rules and lot-testing methods are jurisdiction-specific. For example, Canada applies prescribed tolerances within an average-system framework for consumer prepackaged foods. Check the rules for the market in which your product is sold.[3]
Sample the run, not the prettiest package
One package from the start of a run tells you very little about what happens as a tank empties or a filler warms into its rhythm. Build a small, repeatable sampling plan that captures packages early, middle, and late in the run. Within each window, choose samples without cherry-picking.
For every sample, record the time, package format, gross weight, tare used, calculated net weight, observed foam or fill height, and any relevant tank or filler observations. If you are converting mass to volume, record the density method and value too. Random selection matters in formal package inspection because a non-random sample can undermine the result; the same discipline makes internal trend checks more honest.[2]
A short checklist keeps the team focused:
- Weight holds; visual height moves: investigate foam behaviour, settling time, container geometry, and what the fill-level sensor is actually seeing.
- Weight trends down through the run: look upstream at tank level, headspace condition, transfer stability, and any change in product or line conditions.
- Individual weights scatter: inspect filler timing, valves, seals, package handling, and the measurement method before making broad adjustments.
- Only one format is affected: verify that format-specific parts, tare, and fill-height references are correct.
Follow the drift before changing settings
Foam and short fills often travel together, but they are not the same fault. A change in product temperature or transfer conditions can encourage gas breakout. Turbulence, a tired valve, inconsistent package handling, or a fill-control issue can also create foam or variable delivery. A tank pressure reading is useful process information, but it is not a direct measurement of dissolved CO₂. Pressure and temperature help describe equilibrium conditions; verify carbonation separately with a suitable calibrated method and sampling procedure.[1]
Tank depletion adds another wrinkle. As liquid level falls, hydrostatic contribution changes, so keeping a single headspace condition does not automatically keep every downstream condition identical. That is why a weight trend across the run is more useful than an assumption based on the first few packages.
Where those checks point specifically to upstream pressure drift, PacWizz is one option to consider, not a cure-all for filler faults. Its packaging configuration adds replacement gas to tank headspace; its foot setup uses a bottom-of-tank pressure reading to guide those additions, while its arm setup does not compensate for hydrostatic pressure. It does not replace net-content checks, foam diagnosis, or filler maintenance.[4]
The maker’s move is to treat an almost-full package as an invitation to measure. Weigh representative packages, apply a sound tare, validate density when converting to volume, and compare early, middle, and late results. Once the trend is visible, you can solve the actual packaging problem instead of chasing the foam.