Guide
Carbonation Temperature and Pressure: Why a Gauge Reading Is Not the Whole Story
Learn why pressure alone cannot define carbonation, how product temperature shifts CO₂ equilibrium, and what to measure for repeatable batches.
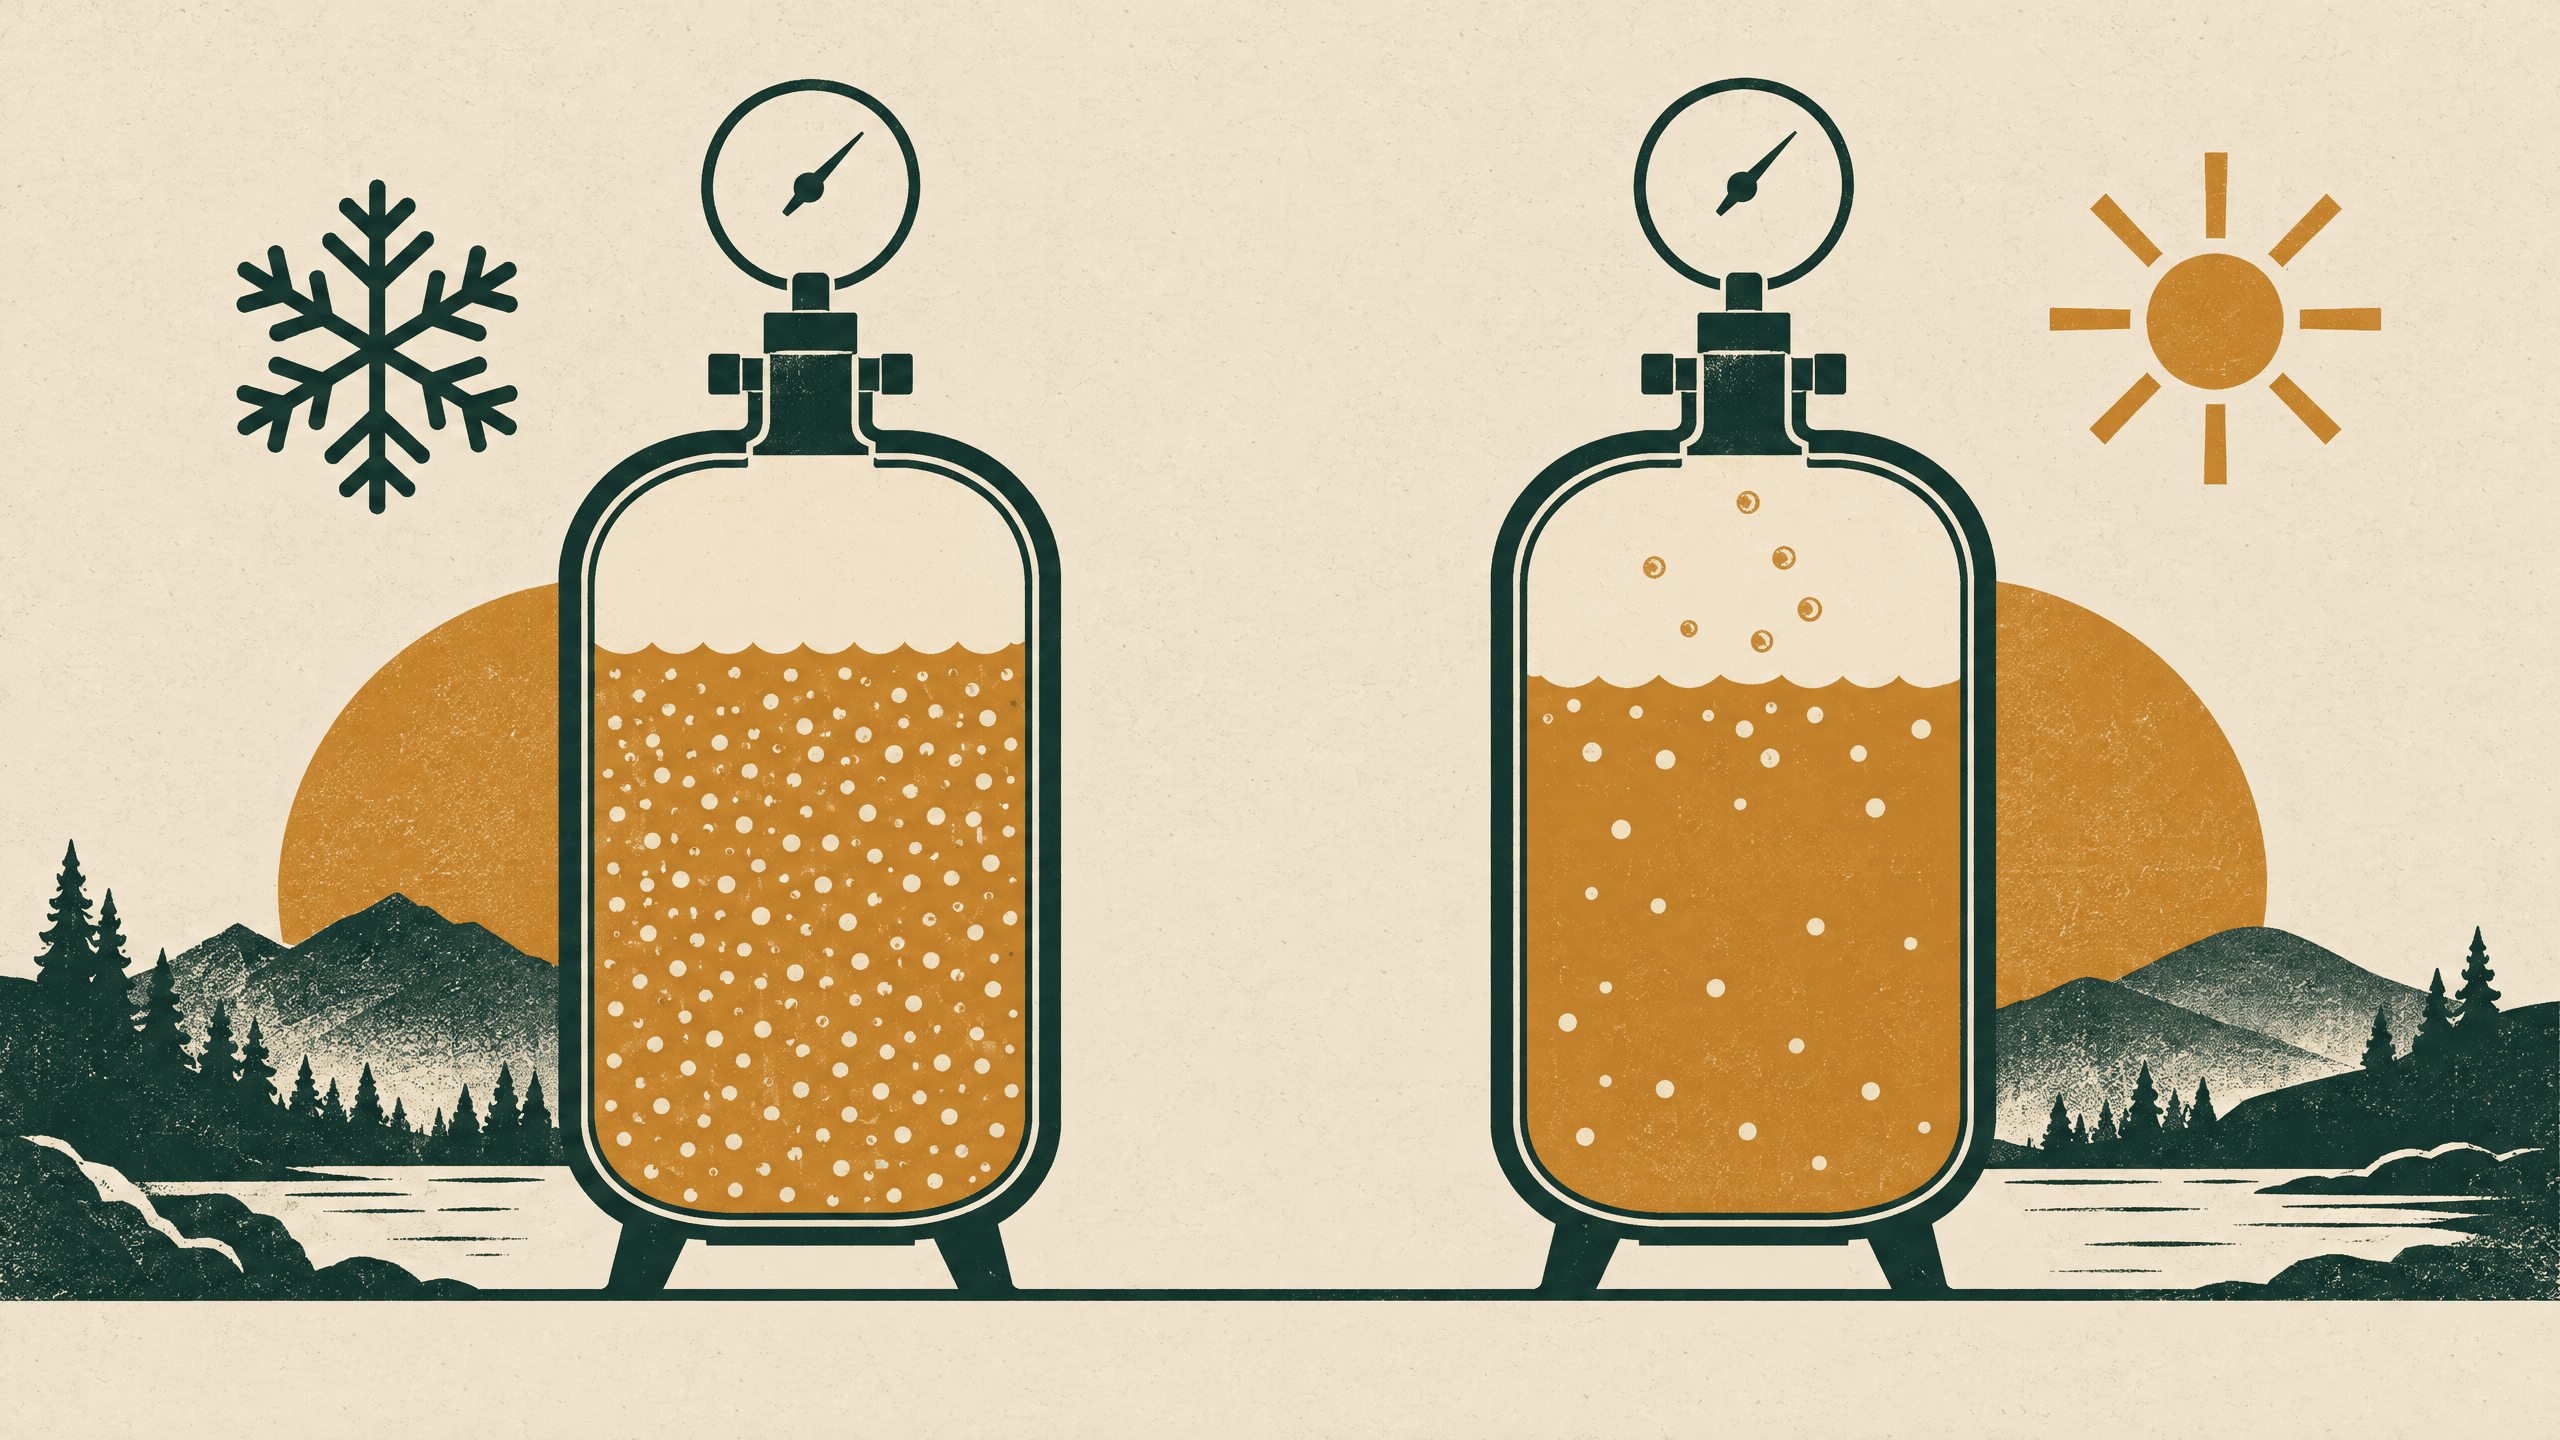
A regulator setting can look reassuringly definite. Set a pressure, wait, and expect the same lively pour every time. In a real tank, though, pressure is only one part of the carbonation picture. Product temperature, the CO₂ in the headspace, and time for gas-to-liquid transfer all matter. Treating one gauge reading as the whole answer is how a repeatable process starts to wander.
The equilibrium question: how much CO₂ can the liquid hold?
Carbonation is dissolved carbon dioxide. At equilibrium, the amount held in the liquid is governed by the conditions on both sides of the gas–liquid boundary. A useful starting point is Henry’s law: at moderate conditions, dissolved gas relates to its partial pressure above the liquid. In plain terms, the relevant pressure is the CO₂ portion of the headspace, not simply every unit of pressure shown on a tank gauge. NIST’s reviewed CO₂–water correlation explicitly uses CO₂ partial pressure and a temperature-dependent Henry’s constant.[1]
That distinction matters when headspace contains gases other than CO₂. A total gauge reading cannot, by itself, reveal the CO₂ partial pressure. It also cannot reveal how much CO₂ is already dissolved in the product. It tells you a condition in the vessel, not the finished carbonation result.
Temperature changes the equilibrium as well. Colder liquid can hold more CO₂ at the same CO₂ partial pressure; warmer liquid needs a higher CO₂ pressure to reach the same equilibrium level. This is why the same carbonation pressure can produce a different outcome after a change in product temperature. It is not a minor seasonal detail or a quirk of one beverage style; it follows from the temperature dependence of CO₂ solubility.[1]
A carbonation pressure chart can be a useful reference, but only when its stated liquid temperature and product basis match the batch in front of you. Read it as a temperature-linked estimate, not a universal tank instruction. If the liquid is warmer or colder than assumed, the chart’s pressure relationship has moved with it.
The rate question: how quickly does CO₂ get there?
Equilibrium describes the destination, not the journey. A tank may have conditions that support a chosen equilibrium carbonation level yet still need time to approach it. Chemical-engineering mass-transfer models separate these ideas: thermodynamics predicts equilibrium, while mass transfer describes how quickly a process reaches it. The rate depends on the driving force and the available gas–liquid contact, among other operating conditions.[2]
For makers, that is the practical reason not to assume that colder product automatically means a faster carbonation step. Cooling increases the equilibrium capacity for CO₂, but the route to that equilibrium still depends on the system. Gas–liquid contact, stone condition, mixing, installation, and the gap between the current and desired state all shape the time needed.
A carbonation stone deserves the same care. Its wetting pressure, the liquid’s hydrostatic contribution, and vessel conditions all affect gas delivery. Do not borrow a regulator setting from another tank or attempt to force a disconnected stone beyond its rating. Work within the vessel and component manufacturers’ procedures, with relief protection and the site’s CO₂ safety practices in place.
Measure the liquid, then verify the result
Room temperature and the outside of a vessel are not interchangeable with actual product temperature. For dependable decisions, record the product temperature at the point your procedure specifies, along with the tank condition and the elapsed hold time. That gives the team a meaningful basis for comparing batches rather than trying to interpret a number stripped from its context.
Then separate process control from verification. A temperature-and-pressure reading, or a controller that uses those inputs, can set or hold process conditions; it is not a direct measurement of dissolved CO₂. The American Society of Brewing Chemists’ dissolved-CO₂ method establishes partial gas pressures in the container at a particular temperature, and also describes an instrumental volume-expansion approach for brewery products.[3] Use a suitable calibrated method and representative sampling procedure to confirm the actual dissolved CO₂ level for your product.
This protects diagnosis. If a batch is not where you expect, first ask whether the temperature record, headspace conditions, and verification sample describe the same moment in the process. Only then investigate transfer and equipment factors. A pressure change made without that context may hide the cause rather than fix it.
A steadier carbonation check
Before changing a carbonation condition, pause for a short, repeatable check:
- Confirm the product temperature, not just the room or tank-skin temperature.
- Note the tank pressure and whether it represents a CO₂-rich headspace or a mixture of gases.
- Check that the batch has had the intended, documented time and gas–liquid contact conditions.
- Inspect connections and transfer hardware under your approved SOP; keep stones clean, correctly installed, and within rating.
- Verify dissolved CO₂ with the calibrated method and sampling practice your operation uses.
The useful habit is simple: pair every pressure observation with product temperature, then distinguish the conditions you control from the carbonation you verify. That small discipline turns a gauge reading from a guess into part of a dependable making record.